If you’ve ever ordered prescription meds from a pharmacy, you’ve probably seen those neat individual plastic blisters holding vials, pills, or ampoules—think the ones that pop easily when you press them with your thumb, keeping each dose sterile and clearly labeled. As a medical blister packaging machine supplier, I get asked this question all the time: “How does that machine actually handle vials specifically?” It’s not just shoving a vial into a plastic bubble, promise. There’s a lot of careful, precise steps that go into making sure every vial ends up sealed right, safe for patients, and ready to make it to the pharmacy or clinic without issues. Medical Blister Packaging Machine
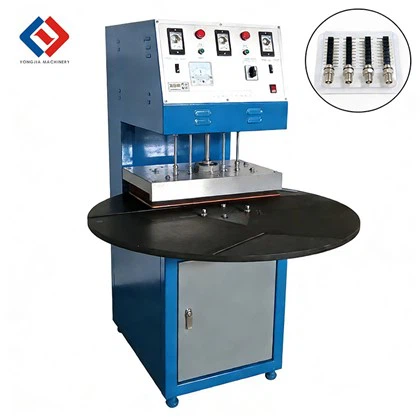
First, let’s cut through the jargon and get real: vials are tricky. Unlike pills or flat ampoules, they’re rigid, cylindrical, and often glass (sometimes plastic for specialty meds), so they don’t fit into generic blister cavities. A blister machine built for small pills can’t just swap out parts for vials—you need a machine designed for the job, or at least with interchangeable tooling. When someone reaches out to me for a machine to package vials, the first thing we talk about is their vial specs: size (obviously, a 2ml insulin vial is way different from a 20ml vaccine vial), material (glass vs. plastic), and whether the vial has a cap, rubber stopper, or is open at the top. Those details determine every single step the machine will follow.
Let’s walk through the process step by step, like we’re standing next to the machine on a factory floor (no boring textbook stuff, I swear). The first step is loading the vials, and yeah, that’s not as simple as pouring them in. Most of the machines we supply use a vibratory feeder, which is basically a bowl that vibrates so the vials line up in a single file, all facing the same direction. Wait, important: vials have tops and bottoms, right? If you load them upside down, you’re wasting time and risking contamination. The feeder has little tracks and sensors that flip or reorient any vial that’s facing the wrong way. Some of the more high-speed models (for clients packaging thousands of vials an hour) even use visual cameras to check each vial’s orientation before it moves on—if it’s backwards, the machine will just reject it, no manual sorting needed. That’s a big one for cutting down on downtime, because reworking misaligned vials is a total pain.
Next up, we’re prepping the blister film. Blister packaging uses two main parts: the clear top film (usually PVC or a specialty medical-grade plastic) that’s heated and molded into cavities, and the lidding foil (aluminum, mostly) that seals the back, with the printed labels or dosage info. For vials, the cavities in the clear film need to be deep enough to hold the whole vial, plus they need to be custom-shaped so the vial doesn’t rattle around during sealing or shipping. The machine takes the clear film, feeds it through a heating station—nothing too hot, just enough to make the plastic soft and moldable—then uses a set of custom punches to press the heated film into cavities that match the client’s vial size. If the client has 10 different vial sizes, we can swap out those punches in like 15 minutes, no tools required, which is a huge win for small pharma companies that package multiple meds.
Wait, here’s a thing people don’t always realize: vials aren’t just dropped into cavities. Because they’re rigid, if you just drop them in, they might shift when you seal the lidding, which can mess up the label or even leave the vial unsealed. So after the cavities are molded, the machine has a pick-and-place unit—usually a set of soft, rubberized grippers that don’t scratch the vial’s glass or plastic surface—that takes each aligned vial from the feeder and sets it straight into the center of its cavity. The grippers are calibrated for pressure, too; if they squeeze too hard, they can crack a glass vial, and if they don’t squeeze enough, the vial falls out. I’ve had clients come to us after buying a cheap overseas machine that cracked 1 out of every 50 vials because the gripper pressure was off, so we make sure all our machines have adjustable pressure settings so that doesn’t happen.
Once the vial is sitting nice and secure in its cavity, it’s time to check for errors. This is where quality control (QC) kicks in, and it’s non-negotiable for medical packaging. The machine has a bunch of sensors: first, a light sensor that checks if there’s actually a vial in each cavity (no empty spots, that would mean a lost dose). Then, a vision system that checks two things: is the vial sitting straight, not tilted? And did the feeder drop the wrong vial size by mistake? If either of those is off, the machine automatically ejects that blister segment before it goes any further. Some of our clients also add a weight check—since vials have consistent weights, a weight sensor can pick up if a vial is missing or underfilled, which is another layer of QC. For meds that need to stay sterile, we also make sure the whole vial handling area is enclosed and has a HEPA air filter, so there’s no dust or contaminants getting on the vials during processing. That’s a requirement for all medical packaging, right? We don’t cut corners on that.
Next step is sealing the blister. For vials, we use heat-sealing, usually with the lidding foil that has a layer of heat-activated adhesive. The lidding film is fed in from a roll, just like the clear blister film, and it’s printed with all the required info: lot number, expiration date, dosage, drug name, all that FDA or local regulatory stuff. Wait, side note: we make sure all our machines are set up to work with variable data printing, so clients can print unique lot numbers on every single blister, which is mandatory for traceability. Now, when it comes to sealing, you can’t just press heat anywhere—you need to heat the edges of the blister cavity, not the middle where the vial is, because that could damage the vial’s rubber stopper or even break it. The machine uses a heated die that matches the shape of the cavity, so it only applies heat and pressure to the perimeter of the blister. The temperature, pressure, and sealing time are all adjustable too—different plastics and vial materials need different settings. For example, glass vials might need a slightly higher temperature than plastic vials, because plastic can warp if it’s too hot, and glass needs enough heat to make the adhesive stick. We test all the settings with the client’s exact vials when we set up the machine, so we don’t have to guess.
After sealing, we need to cut the blister into individual units, right? Most medical blister packaging for vials is cut into strips or individual blisters, depending on what the client needs. The machine has a rotary cutting tool or a flatbed cutter that trims the lidding and blister film into the desired size. For vials, we use a sharp, medical-grade cutting blade that makes a clean cut—no ragged edges that could tear the packaging, which would break the sterility. Also, the cutting is aligned with the cavities, so each individual blister holds exactly one vial, no overlaps or gaps. Some clients want the blisters on a roll, for automated dispensing machines in hospitals, so we can adjust the cutting to leave perforations between blisters, so you can tear off one vial easily without pulling the whole roll.
Wait, what about after cutting? There’s one more step I almost forgot: checking the seal. Even after all that, sometimes a seal is weak, which would let moisture or contaminants in, or even let the vial fall out during shipping. Our machines have a leak test, usually a vacuum test, where they pull a little air out of each individual blister and check for air leaks. If a blister doesn’t hold pressure, the machine will reject it. That’s super important for vials, because if a seal breaks, the medication inside can go bad, and that’s a safety hazard for patients. I’ve seen clients lose big contracts because they had untested seals and vials got damaged in transit, so adding that leak test is non-negotiable, not an extra feature we push.
Now, let’s talk about downtime, because that’s the #1 complaint we hear from clients. Medical packaging lines can’t stop every 10 minutes because a vial got stuck. The machines we supply are designed for minimal changeover, too—like I said earlier, swapping punches for a new vial size takes 15 minutes or less, no special tools. We also have a bunch of sensors that catch jams before they turn into big problems. If a vial gets stuck in the feeder, the machine alerts the operator with a exact error message, like “Vial jam at position 12” instead of just “Error,” so someone can fix it fast. That saves a ton of time, which means more vials packaged per hour, which means more revenue for the client.
Wait, I should also mention regulatory stuff, because this is medical packaging, not candy. All the machines we sell are compliant with FDA 21 CFR Part 11 for electronic records and signatures, and meet ISO 13485 standards for medical device manufacturing. We also provide validation documentation for every machine, so clients can prove to regulators that their packaging process is safe and consistent. A lot of small pharma companies don’t realize that buying a cheap, uncertified machine will get them stuck in audits, so that’s a big part of what we offer that other suppliers don’t.
Let me wrap this up with a real example, just to make it concrete. Last year, we worked with a small biotech that was packaging 5ml plastic vials of a new monoclonal antibody. Before they found us, they were using a general-purpose blister machine that cracked 3% of their vials and had a seal error rate of 1.2%, which was way too high for their clinical trial meds. We swapped out their grippers for pressure-adjustable soft rubber ones, customized the cavity punches for their 5ml vials, added the visual orientation camera and leak test, and adjusted the sealing settings. After setup, their crack rate dropped to less than 0.1%, and seal errors were almost zero. They now package 1,200 vials an hour, which is double what they were doing before, and they passed their FDA audit on the first try. That’s the stuff that matters, right? It’s not just a machine—it’s a tool that keeps meds safe, gets them to patients, and makes the client’s job easier.

If you’re a pharma manufacturer, clinical trial lab, or anyone packaging vials for medical use, and you’re tired of machines that jam, crack vials, or don’t meet regulatory requirements, hit me up. We’ll walk through your specific needs, customize a machine that fits your vial sizes and production rates, and make sure every step is compliant and reliable. No pushy sales stuff, just straight talk about what your operation actually needs.
Head Foot Operated HF Welding Machine REFERENCES
- European Medical Devices Regulation (MDR) Annex VIII: Requirements for Packaging and Labeling of Medical Devices
- FDA 21 CFR Part 11: Electronic Records, Electronic Signatures
- ISO 11607-1: Packaging for Terminally Sterilized Medical Devices – Part 1: Requirements for Materials, Sterile Barrier Systems, and Packaging Systems
- Pharmaceutical Packaging Technology: Blister Packaging for Parenteral Vials, Journal of Pharmaceutical Innovation, 2022
Dongguan Yongjia Machinery Equipment Co., Ltd.
We are one of the most reliable medical blister packaging machine manufacturers and suppliers in China, specialized in providing high quality customized service. Please feel free to wholesale advanced medical blister packaging machine at low price from our factory. For quotation, contact us now.
Address: No. 240, Chashan South Road, Chashan Town, Dongguan City, Guangdong Province, China
E-mail: info@yjwelding.com
WebSite: https://www.yjhighfrequencymachine.com/
